A seal is the cheapest part on most bills of materials and one of the most common causes of a returned unit. A leak at an autoclave door, water inside an outdoor enclosure, a sensor that fails after a season of UV: the trail usually leads back to one component specified in a hurry. Buyers who qualify as a custom silicone seal manufacturer properly spend less later.
Six checks decide the outcome. Does the supplier understand your sealing conditions, or only the drawing? Does its material knowledge go past the word “silicone”? Can it make the format you need, whether that is a strip, a tape, a ring, or a gasket? Can it hold dimensions and hardness from sample to batch, and will it say when a design will not seal? Price ranks after all six.
This guide works through those checks in the order that decides most projects.
Why silicone seals fit some jobs and fail in others
Silicone suits seals that must survive heat, cold, weathering, repeated cleaning, or contact with food and skin. It fails where the seal must resist abrasion, extrusion under pressure, or long contact with fuels, oils, and concentrated acids.
VMQ silicone holds a published service range of roughly −60°C to +230°C, wider than nitrile, EPDM, or natural rubber. It resists ozone and UV, and it is inert enough for skin and food contact.
The limits matter as much. Lower tear strength means silicone copes badly with sharp edges, abrasive media, or high-pressure dynamic service. Standard VMQ also swells in many hydrocarbon fluids, which is why fluorosilicone grades exist. For a hydraulic rod seal under pressure, silicone is the wrong answer, and a competent supplier says so.
The compounds you will be asked about
- VMQ, methyl vinyl silicone. General purpose and food contact, usually platinum-cured.
- FVMQ, fluorosilicone. Fluorine on the backbone for fuel and oil resistance, at a higher cost.
- PVMQ, phenyl silicone. Pushes the low-temperature floor down for cryogenic work.
- LSR, liquid silicone rubber. A two-part liquid, injection molded, for thin-walled parts.
- HCR, high-consistency rubber. A solid compound for compression molding and extrusion.
Peroxide cure is cheaper and fine for most industrial work.
The four silicone seal formats and how each is produced
The format sets the production route, the tooling cost, and the tolerance you can hold. A silicone seal strip, a silicone seal tape, a silicone seal ring, and a silicone seal gasket are made in four different ways, and asking for the wrong one inflates cost or caps quality.
Silicone seal strip
Extruded with a constant cross-section, then cut to length. Sections can be round, square, D-shaped, or bespoke. The die is far simpler than a mold, so long strips are cheap, but tolerance comes from the die and the curing line. Strips are often joined into a loop with a vulcanized splice.
Silicone seal tape
A flat product: a slit roll, or a die-cut length from a sheet. Thickness is the main dimension and carries a standard sheet tolerance. Adhesive backing handles enclosure sealing where the tape also fills a gap, and standard shapes need no tooling.
Silicone seal ring
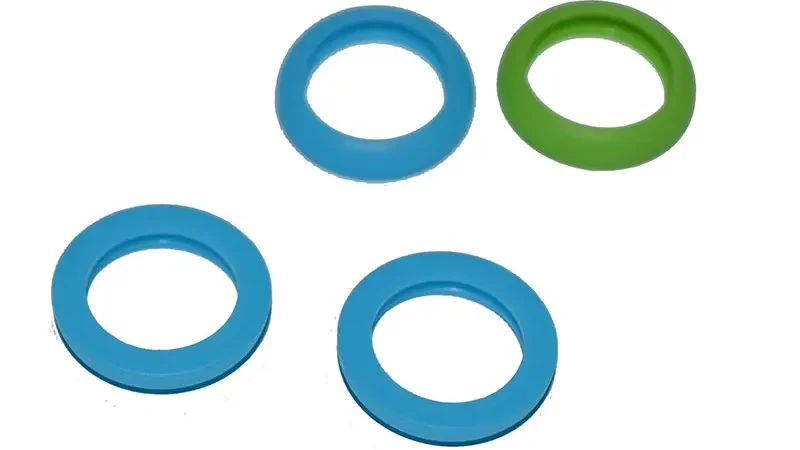
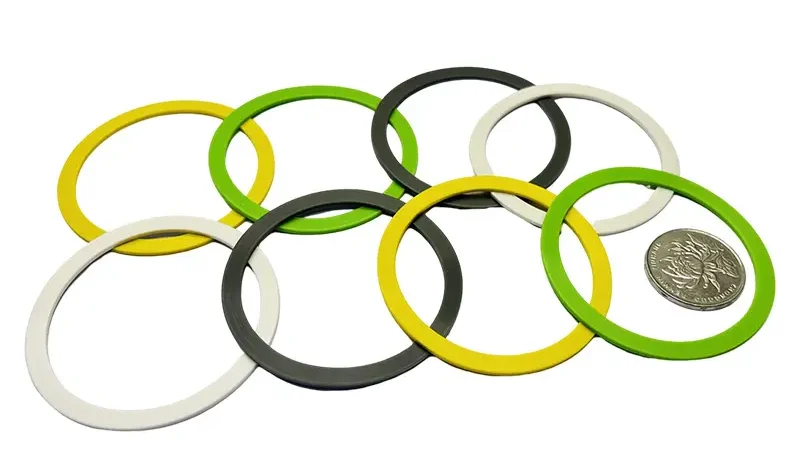
Either molded to shape or cut from extruded cord and joined. Molded rings cover O-ring cross-sections and custom profiles with close control of inner diameter. Cut-and-joined rings need no tooling and suit large diameters such as a tank lid.
Silicone seal gasket
Usually a flat part, die-cut from a sheet. With no cavity tooling, die cutting wins on low and medium quantities and on large footprints. A three-dimensional profile, a lip, or a groove with controlled compression moves the part to compression molding.
| Format | Production route | Specify | Common use |
|---|---|---|---|
| Silicone seal strip | Extrusion, cut to length | Cross-section drawing, length, splice method, hardness | Door and window seals, enclosure edges |
| Silicone seal tape | Sheet slit or die-cut | Thickness, width, adhesive type | Panel sealing, gap filling, enclosure covers |
| Silicone seal ring | Molded, or cord cut and joined | Inner diameter, cross-section, hardness, splice position | Flange joints, lids, fittings |
| Silicone seal gasket | Die-cut flat, molded if profiled | Outline, thickness, compression target | Flat flanges, covers, sanitary fittings |
What to define before you contact a supplier
Write down what the seal has to do before you ask for a quote. Suppliers quote from the information they receive, and a thin inquiry produces a quote that assumes the cheapest possible interpretation.
- Drawing or 3D file, or a sample if no drawing exists.
- Format and the mating surface the seal sits against.
- Hardness in Shore A, or the compression behavior you need.
- Temperature range, including peaks during cleaning.
- Contact media: water, steam, food, cleaning chemicals, oils.
- Groove dimensions and how the seal is retained.
- Compliance requirements, with the certificates you expect.
- Prototype and production volumes, inspection needs, and packaging.
The details that move the quotation most
Volume and format set the floor; hardness, tolerance, and compliance set the rest. A tight tolerance class costs more than a standard one, and a food-contact compound costs more than a general-purpose one.
How to read a supplier’s material claims
Ask for the material specification, not the marketing page. A credible supplier can send an ASTM D2000 line call-out for the compound it intends to use, a datasheet for the batch it will run, and an explanation of what each segment means for your part.
Material names carry almost no information. Two compounds are both sold as 70 Shore. A silicone can differ in compression set, heat-aging behavior, and swelling in a given fluid, and those differences decide whether a seal holds for a season or for years. ASTM D2000 encodes grade, heat-resistance class, hardness, and tensile strength, plus suffix tests.
- “Why this compound instead of the alternative?” A supplier that understands your conditions talks about temperature, media, and compression. One that does not talk about stock.
- “Which batch will this come from, and can I see its test record?” A datasheet for a generic compound proves nothing about the part in the box.
Matching the manufacturing process to your seal
Match the process to geometry, volume, and tolerance rather than to what the factory already runs. Extrusion, die cutting, compression molding, and LSR injection Molding each win in a different corner of that space.
A continuous cross-section means extrusion. Flat and large means die cutting. Profiled with moderate volume means compression molding. Complex, thin-walled, or tight-tolerance means LSR injection molding.
| Your situation | Process that usually fits | Why |
|---|---|---|
| Long constant profile, any quantity | Extrusion | Simple die, no cavity tooling |
| Flat part, low to medium volume | Die cutting | No tooling, fast turnaround |
| Profiled or thick part, 3D geometry | Compression molding | Handles solid compounds and thick sections |
| Small precision part, thin walls | LSR injection molding | Closed-loop control, flash-free |
| High volume with overmolded inserts | LSR injection molding | Automated cycles, in-mold bonding |
Die cutting and extrusion put tolerance on the raw material and the cutting die, so expect injection-molding precision there only after demonstration.
Quality systems, test reports, and traceability that mean something
A working quality system shows up as records, not certificates. The supplier you want can describe what it checks at incoming, in-process, and final inspection and can name the test method behind every number on the report that ships with your parts.
The European Sealing Association keeps a public technical library on sealing device standards, testing, and materials, a useful check on whether a supplier’s quality vocabulary matches the industry’s.
Incoming inspection asks whether the raw compound is the specified compound and whether the batch certificate is present. In process, look for hardness checks at defined intervals and recorded molding parameters. Final inspection should show dimensional measurement against your drawing, visual criteria for flash, and a lot number tying parts back to the incoming batch.
The tests that appear most often:
- Hardness, by durometer. Compared first, understood least.
- Compression set, which predicts whether the seal still pushes back after a year under load.
- Tensile strength and elongation at break, which show how the compound handles installation stress.
- Heat aging, which shows behavior after extended service.
Two documents matter most: a certificate of analysis stating measured values for the batch and a dimensional report for the finished parts with the measurement method.
Tooling, samples, and the first-article approval loop
Get the design reviewed before the mold is cut. Most of the cost of a badly designed silicone seal is created in the tooling decision, and nearly all of it can be avoided in a review that takes days instead of weeks.
A design-for-manufacturing review covers wall thickness, parting line position, the draft needed to release the part, where flash is likely to form, and whether the sealing lip can be molded without undercuts. Findings should come back in writing.
- Freeze the drawing after review, and record every change in writing.
- Approve a first-article sample, measured against the drawing, before production tooling is committed.
- Test the sample in the real assembly, not on a bench.
- Confirm tool ownership, free modification rounds, and who pays for later changes.
- Agree on what happens when production parts fall outside the approved sample.
Samples that pass followed by production that drifts are the failure buyers complain about most, and the fix is a written definition of acceptable variation.
Compliance by market: food, medical, water, and automotive
Different markets require different evidence, and “we can make food grade” is not evidence. Ask for the document behind the claim, and check that it names the compound rather than the factory.
| Target market | Standard or framework | Evidence to request |
|---|---|---|
| Food contact | FDA 21 CFR 177.2600, LFGB, EU 10/2011 | Compliance statement naming the compound and its cure system |
| Medical devices | ISO 10993, USP Class VI | Accredited lab reports, sterilization compatibility statement |
| Drinking water | NSF-51, or the National Potable Water Scheme | Current listing covering the compound |
| Automotive and electronics | IATF 16949, UL flammability ratings | Certificate scope, PPAP on request |
| All markets | REACH, RoHS | Declarations covering the compound and its additives |
Compliance is a chain. The certificate covers a compound. That compound has to be the one used for your part. The part has to come from the batch on the paperwork.
What drives cost, MOQ, and lead time?
Cost comes from tooling, material grade, tolerance class, and inspection intensity. Minimum order quantity follows from how that tooling is amortized. Lead time comes from mold making, sampling, and your own approval speed, in that order.
Tooling is the largest single variable. Cavity count, mold steel, part size, and surface finish all push it up, and a multi-cavity hardened tool for LSR costs far more than a single-cavity compression mold. Material grade comes second, and tolerance class third, because tighter tolerances mean more process control and more inspection.
MOQ is a recovery mechanism, not a fixed number. A low minimum usually means the tooling cost is recovered through the unit price or amortized across a volume commitment. Ask for the unit price at twice and at five times your planned volume, and the structure becomes visible. Lead time splits into making the tool, running samples, and winning your own approval, which buyers consistently underrate.
Red flags and how to run a short supplier trial
Walk away when a supplier copies the drawing without asking about the application, outsources every non-standard job, or cannot describe how it tests. Run a short trial before you commit: one part, one drawing, and full records on the finished samples.
- The drawing is the only thing discussed. No questions about temperature, media or compression.
- Non-standard work is always subcontracted, putting the schedule and tolerance in someone else’s hands.
- Sample and production compounds differ, with no written record of the change.
- Material data sheets are refused, or one generic sheet serves every compound.
- Every question gets a yes. A supplier that never pushes back is either not reading the design or not planning to follow it.
A short trial answers more than a factory tour. Send one drawing for a silicone rubber sealing ring, ask for samples in two hardness levels, request the dimensional and hardness reports with them, then compare the second batch against the first.
FAQ
How can I tell whether a silicone seal uses virgin compound or regrind?
Not by eye, but you can gather evidence. Ask which compound is specified and whether regrind is permitted at all, then check the batch certificate of analysis. Appearance gives weak signals: virgin platinum-cured silicone is usually uniform in color and recovers quickly after stretching, while heavily filled or reground material often looks dull and returns slowly. For a critical seal, ask for a spectroscopic check against the reference compound.
What decides the minimum order quantity for a custom silicone seal?
Amortization of tooling, plus the supplier’s minimum run for the process. Die-cut and extruded seals carry little or no tooling, so minimums are usually set by material handling and stay low. Molded parts carry a mold, and the minimum is set so the mold cost spreads across enough units to suit both sides. Where volume is low and geometry allows it, a cut-and-joined ring moves the project into a lower-minimum process.
Can a silicone seal be bonded directly to plastic or metal?
Yes, usually with self-bonding liquid silicone rubber molded onto the substrate in the same cycle. The insert needs surface preparation and, depending on the material, a primer. Bonding works best when the substrate choice is made early, because some plastics and metals bond to silicone far more reliably than others, and the bonding area gets decided at the mold design stage.